


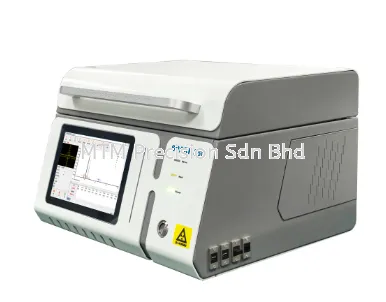


Benetech GT-1201 for Incoming Inspection and Supplier QC Malaysia

Benetech GT-1201 for Incoming Inspection and Supplier QC Malaysia
Your supplier delivers painted or powder-coated metal parts to your factory.
The parts look good.
But how do you know whether the coating is consistent with previous batches?
For Malaysian manufacturers that outsource painting, powder coating or metal fabrication, incoming inspection can help detect problems before the components enter production or are delivered to customers.
A portable Benetech GT-1201 coating thickness gauge can support incoming QC by allowing personnel to check suitable coated metal components and compare measurements across parts, batches and suppliers.
Why Check Coating Thickness During Incoming Inspection?
Many factories inspect incoming components for:
Dimensions
Quantity
Colour
Surface defects
Scratches
Dents
Workmanship
But coating thickness may receive less attention.
A component can look visually acceptable while its coating thickness differs significantly from previous production.
If coating thickness is important to your product specification, incoming inspection provides an opportunity to identify the issue before the parts move further into production.
Which Incoming Parts Can Be Checked?
Potential applications include suitable:
Powder-coated steel cabinets
Painted steel panels
Aluminium enclosures
Machine covers
Metal brackets
Fabricated frames
Electrical panels
Industrial housings
Automotive metal components
Other coated metal parts
Suitability depends on the coating, substrate, component geometry and measurement requirement.
Do not assume every coated component can be measured in exactly the same way.
Example: Outsourced Powder Coating
Suppose your company manufactures electrical cabinets.
You fabricate the steel internally but send the cabinets to an external powder coating supplier.
When the finished cabinets return, they look acceptable.
Instead of checking only colour and appearance, incoming QC can also measure selected locations.
For example:
Door – Top
Door – Centre
Door – Bottom
Side panel – Centre
Rear panel – Centre
The results can then be compared with your internal requirement or previous accepted batches.
Do Not Measure Only One Part
Suppose a delivery contains 500 coated components.
Measuring one random point on one component gives very limited information.
A better incoming inspection procedure should define a suitable sampling plan according to your quality system.
The selected samples can then be measured at consistent locations.
The objective is to obtain representative information about the incoming batch.
Use the Same Measurement Locations
Consistency is important.
If today's inspector measures the centre of the panel but next month's inspector measures directly beside an edge, comparing the results becomes less useful.
For repeat components, create a simple measurement map.
For example:
A – Upper left
B – Upper right
C – Centre
D – Lower left
E – Lower right
Use the same points where practical.
This makes supplier comparison much more meaningful.
Compare Current Batch with Previous Batch
One of the strongest uses of coating thickness data is trend comparison.
Suppose Supplier A has delivered the same component for six months.
Previous accepted batches showed a consistent measurement pattern.
A new shipment suddenly shows substantially different readings.
That does not automatically mean the shipment must be rejected.
But it provides a reason to investigate.
Ask:
Has the coating process changed?
Has the material changed?
Was another coating supplier used?
Is the substrate different?
Is the measurement procedure still the same?
The GT-1201 can help reveal the change.
Supplier A vs Supplier B
Imagine your company is evaluating two powder coating suppliers.
Both provide visually acceptable products.
Price is similar.
Delivery time is similar.
How else can you compare them?
Coating thickness consistency can become one additional supplier-quality indicator.
For example, you may compare:
Supplier A – Batch 1
Supplier A – Batch 2
Supplier A – Batch 3
against:
Supplier B – Batch 1
Supplier B – Batch 2
Supplier B – Batch 3
The objective is not simply to identify which supplier applies the thickest coating.
Thicker is not automatically better.
The more useful question is:
Which supplier consistently meets the required specification?
Too Thin Is Not the Only Problem
Incoming QC should not only look for coatings that are below specification.
Coatings that are unnecessarily high may also indicate process variation.
If your requirement has an acceptable range, evaluate the measurement against that range.
The objective should be:
Within specification
rather than:
As thick as possible.
What If One Component Is Very Different?
Suppose nine components show a similar measurement pattern.
The tenth component is substantially different.
Do not ignore it.
Repeat the measurements.
Check several locations.
Confirm:
Surface condition
Measurement position
Substrate
Component geometry
If the difference remains, separate the component for further investigation according to your QC procedure.
What If the Entire Batch Is Different?
This is more significant.
Suppose a new delivery consistently shows a different coating thickness pattern from previous accepted batches.
Before contacting the supplier, verify:
The GT-1201
Measurement procedure
Measurement locations
Base material
Product revision
If these remain consistent, you now have useful measurement evidence to discuss with the supplier.
Use Data Instead of Saying “The Coating Looks Thin”
This is one of the biggest advantages of measurement.
Compare these two supplier complaints.
Complaint A
“Your powder coating looks thinner than before.”
This is subjective.
Complaint B
“We measured the same five QC locations across selected samples from this batch and found a consistent difference compared with our previous accepted batches.”
This provides a much stronger basis for technical discussion.
Measurement data improves communication between purchasing, QC, production and suppliers.
Record the Supplier Name
If multiple suppliers produce similar components, include supplier information in your records.
A simple coating inspection record may contain:
Date
Purchase order
Supplier
Part number
Batch
Substrate
Coating
Measurement location
Thickness reading
Inspector
Over time, this data can become useful for supplier evaluation.
Record the Part Number
Do not combine measurements from different products without identifying them.
Two components may use:
Different steel
Different aluminium
Different coating systems
Different geometries
Different specifications
Keep records linked to the correct part number or product.
Confirm the Base Material
Incoming QC should know what substrate was ordered.
For example:
Powder-coated mild steel
and
Powder-coated aluminium
may look similar after finishing.
But they are different substrates.
If the supplier changes the material unexpectedly, this may also affect your measurement process.
Be Careful with Galvanized Steel
Galvanized components require additional consideration because the structure may involve:
Steel → Zinc → Paint
or:
Steel → Zinc → Powder coating
If your QC requirement is specifically to measure an individual layer, clarify exactly what needs to be measured.
Do not assume a simple coating reading automatically isolates every layer.
Be Careful with Small Parts
Incoming inspection may involve:
Bolts
Nuts
Small brackets
Clips
Fasteners
Small fabricated components
Component size and geometry can influence measurement suitability.
If the available surface is too small or strongly curved, the application should be evaluated before using the GT-1201 as the acceptance tool.
Incoming Inspection of Large Panels
Large flat panels are generally easier to organize into a repeatable measurement map.
For example:
Point A – 100 mm from upper left
Point B – 100 mm from upper right
Point C – Centre
Point D – 100 mm from lower left
Point E – 100 mm from lower right
The exact locations should follow your own QC procedure and product geometry.
The important point is consistency.
Incoming QC Should Not Depend on One Inspector
If only one experienced employee knows how to measure coating thickness, the system becomes difficult to maintain.
Create a simple internal work instruction covering:
How to verify the instrument
Where to measure
How many readings to take
How to record results
What to do with abnormal readings
This improves consistency when different staff perform incoming inspection.
Purchasing Team Can Use the Data Too
Coating thickness data is not only for QC.
Purchasing can use repeated supplier-performance information when evaluating:
Supplier consistency
Quality complaints
Rejection rates
Corrective actions
Supplier changes
This makes the GT-1201 part of a broader supplier-quality process rather than simply a handheld measuring tool.
What If the Supplier Disagrees?
If the supplier disputes your measurement, first make sure both parties are discussing the same:
Specification
Measurement method
Measurement locations
Substrate
Instrument requirements
Acceptance criteria
Two companies can obtain different results if they are not using the same inspection procedure.
For important contracts, agree on the measurement method before mass production begins.
Should You Reject a Batch Based on GT-1201 Readings?
Do not create rejection criteria after the problem occurs.
The acceptance criteria should ideally already be defined by:
Customer specification
Engineering requirement
Purchase specification
Approved QC procedure
or another applicable requirement.
The GT-1201 provides measurement information.
The decision to accept or reject a batch should follow your company's defined quality process.
Incoming Inspection Workflow
A practical workflow can look like this:
1. Receive coated components
↓
2. Confirm part number and supplier
↓
3. Perform visual inspection
↓
4. Select samples according to QC procedure
↓
5. Verify the coating thickness gauge
↓
6. Measure defined locations
↓
7. Record readings
↓
8. Compare with specification and historical data
↓
9. Investigate abnormal results
↓
10. Accept, hold or escalate according to QC procedure
This creates a repeatable inspection system.
Why GT-1201 Can Be Useful for Supplier QC
The Benetech GT-1201 can help suitable incoming-inspection applications move from:
Visual opinion
toward
Recorded measurement data.
It can support:
Batch comparison
Supplier comparison
Incoming QC
Complaint investigation
Production traceability
Supplier performance monitoring
The value comes not only from the instrument itself, but from using it within a consistent inspection process.
Benetech GT-1201 for Incoming Inspection Malaysia
If your company purchases painted, powder-coated or otherwise suitable coated metal components, coating thickness measurement may be worth adding to your incoming QC process.
Before buying the GT-1201, identify:
What coating are you checking?
What is the substrate?
What thickness is expected?
What component geometry is involved?
What specification determines acceptance?
This helps ensure that the instrument matches the actual inspection requirement.
Benetech GT-1201 Supplier Malaysia
MTM Precision Sdn Bhd
Showroom & Service Centre:
No 29-1 & 2, Jalan Bandar 18,
Pusat Bandar Puchong,
47160 Puchong, Selangor, Malaysia
Tel: 03-8080 7172
WhatsApp: +6016-660 7346
Email: mtmpre@yahoo.com
Website: www.mtmpre.com.my
We support manufacturing, fabrication and QC customers throughout Selangor, Kuala Lumpur, Johor, Penang, Melaka, Negeri Sembilan, Perak, Pahang, Kelantan, Terengganu, Kedah, Perlis, Sabah and Sarawak.
If you want to use the Benetech GT-1201 for incoming inspection or supplier QC, send us a photo of the component, together with the base material, coating type and expected thickness, through WhatsApp +6016-660 7346.
We can help evaluate whether the GT-1201 is suitable for your incoming inspection application.
04 Oct 2026
